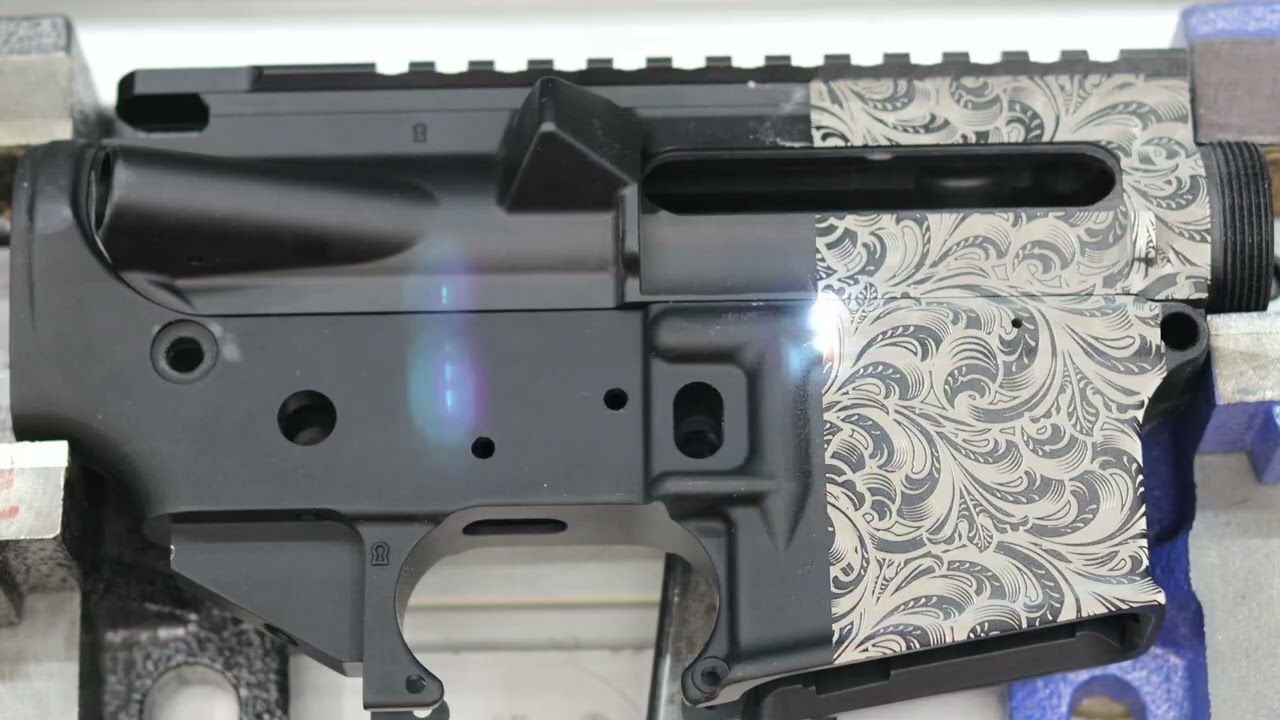
To permanently mark an AR15 lower receiver in compliance with ATF regulations, you need a fiber laser engraver for AR15 work, as only this laser type meets the required metal depth. Unlike other laser types, a fiber laser engraver for AR15 applications removes enough anodized aluminum to create a legally compliant, high-contrast mark. This guide details the exact specifications, legal requirements, and proven settings you need to achieve a durable, ATF-approved engraving on your receiver.
Why you need a fiber laser engraver for AR15 compliance
When the goal is legal firearm marking, a fiber laser engraver for AR15 receivers is the only practical choice because it physically removes metal to meet the ATF's mandatory 0.003-inch depth requirement. CO2 and diode lasers simply cannot achieve this depth on aluminum or steel, making them unsuitable for any serialized or identifying mark. A fiber laser's concentrated beam vaporizes the anodized coating and a thin layer of the underlying aluminum, producing a permanent, readable mark that withstands wear, cleaning, and solvents. If you are engraving a receiver for compliance, personalization, or manufacturing, the fiber laser is the industry-standard tool that guarantees your work is legal and durable.
ATF engraving requirements for firearms
The ATF mandates specific, non-negotiable standards for firearm markings, and knowing them is critical before you begin any engraving project. Federal law requires that the serial number, manufacturer's name, model, caliber or gauge, and city/state of manufacture be permanently marked in a visible area on the firearm's receiver. The engraving must have a minimum depth of 0.003 inches (0.076mm), measured from the original surface, and the serial number and associated license numbers must have a minimum text height of 1/16 inch. These rules apply to all firearms, including AR15 lowers, and failure to comply can result in hefty fines or legal penalties. For your own protection, always verify the latest ATF rulings, as these specifications are strictly enforced and non-negotiable.
Why CO2 and diode lasers fail on AR15 receivers
CO2 lasers are often marketed for their versatility, but they are fundamentally incapable of meeting ATF depth standards on AR15 receivers because they only bleach the anodized dye, turning it white or grey without removing any metal. This leaves a surface-level mark that is not permanent and will wear off with handling, making it useless for legal serialization. Diode lasers, on the other hand, lack the peak power density required to penetrate the hard anodized layer of 7075 or 6061 aluminum, resulting in shallow, illegible marks. The core issue is that both technologies operate at wavelengths that are poorly absorbed by bare metals, meaning they cannot vaporize the material to create a 0.003-inch-deep cavity. For this reason, any attempt to use a CO2 or diode laser for AR15 engraving will produce a non-compliant and temporary result.
How a fiber laser engraves anodized aluminum
A fiber laser engraves anodized aluminum by using a focused beam of light at a wavelength (typically 1064nm) that is readily absorbed by the metal, unlike CO2 lasers. When the beam hits the surface, it rapidly heats and vaporizes the anodized coating and a controlled layer of the aluminum substrate, creating a clean, recessed cavity. This process reveals the lighter, bare aluminum underneath, which contrasts sharply with the darker anodized surface, producing a high-contrast mark that is both permanent and legible. The depth is achieved through multiple passes, each removing a few microns of material, until the required 0.003-0.010 inch depth is reached. Because the laser physically removes material rather than just changing its color, the mark is resistant to solvents, abrasion, and UV exposure, ensuring it remains readable for the lifetime of the firearm.
Recommended fiber laser power: 30W, 50W, or 60W MOPA
For reliable ATF-compliant engraving on AR15 receivers, a minimum of 30W to 50W of fiber laser power is generally required to ensure sufficient depth and speed. A 30W laser can work but will require more passes and slower speeds, which is acceptable for occasional use but inefficient for professional shops. The 50W fiber laser is the most common choice for gun smiths because it offers a strong balance of speed and affordability, easily achieving the 0.003-inch depth in under a minute with proper settings. However, a 60W MOPA (Master Oscillator Power Amplifier) fiber laser is often recommended as the "sweet spot" for firearm engraving because it provides higher peak power and pulse-width control, enabling faster engraving and finer detail on both aluminum and steel. The MOPA's adjustable pulse duration allows you to fine-tune the heat input, reducing the risk of warping thin receiver walls while producing consistent, deep marks. For professionals who want the best combination of speed, precision, and depth, investing in a 60W MOPA is the optimal choice.
Example laser settings for deep engraving on a lower receiver
To achieve a compliant 0.003-0.010 inch depth on a 50W fiber laser, start with these tested settings and adjust based on your specific machine and material. For a standard 50W fiber laser, use a speed of 2000 mm/s, a power setting of 50%, and a frequency of 75 kHz, then run 20 passes to reach the required depth. Alternatively, a slower speed of 3000 mm/s with 40% power and 15-18 passes also works well, but you must verify the final depth with a depth gauge. Always use a high-quality lens with a short focal length (e.g., 125mm or 150mm) to concentrate the beam and increase energy density. After engraving, clean the area with a solvent to remove any residual debris and check the depth with a micrometer or depth gauge, never assume the settings are perfect without measuring. Remember that these are starting points; you may need to adjust power or speed by 5-10% depending on the specific alloy (7075 vs. 6061) and the condition of your laser.
Critical rules for legal firearm engraving
Before you engrave anything, understand that it is illegal to remove, cover, obscure, relocate, or alter an existing serial number or required identification mark on a firearm. This means you cannot grind down or laser off an old serial number and re-engrave it, even if you are the legal owner, doing so violates federal law and can lead to severe criminal charges. Additionally, you must always test your laser settings on a scrap piece of the same anodized aluminum before engraving the actual receiver to avoid ruining a costly part. This test should include the same depth and text height requirements to ensure your final engraving meets ATF standards. Finally, ensure the engraving is placed in a visible area on the receiver (typically the side or above the trigger well) and that the text is at least 1/16 inch tall. By following these rules, you protect yourself legally and ensure your engraving is both professional and compliant.